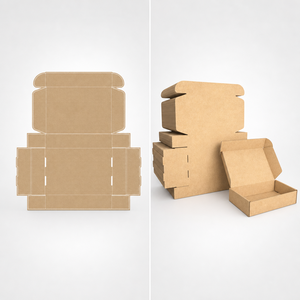
Explore our factory direct production line covering customized barrier zipper pouches, eco-friendly kraft bags, heavy-duty corrugated shipping combos, and retail display packaging engineered to precise technical specifications.
As global enterprise brands transition toward sustainable, high-barrier flexible packaging, selecting an audited, top-tier zipper bag manufacturer is critical. Modern packaging engineering requires strict compliance with oxygen transmission rate (OTR) parameters, water vapor transmission rate (WVTR) limits, hermetic zip lock integrity, and international food contact safety standards.
Our state-of-the-art manufacturing infrastructure utilizes dust-free Class 8 cleanrooms for film blowing, extrusion, printing, and bag making. This guarantees zero particulate contamination for food-grade, pharmaceutical, and high-purity industrial packaging applications.
Every zipper profile undergoes rigorous ASTM F88 seal strength testing and ASTM F2054 burst pressure testing. Our inline ultrasonic and heat-sealing technology ensures air-tight, leak-proof closures capable of enduring severe freight shock and thermal expansion.
From single-track press-to-close zippers, slider zips, and pocket zippers to child-resistant (CR) safety closures, our factory provides limitless customization. Enhance brand presence with spot UV, soft-touch matte, tactile embossing, and foil stamping.
Understanding film structure performance is essential for optimizing product shelf life and ensuring transport stability. Review our technical material matrix engineered for custom zipper bag manufacturing:
| Film Laminate Structure | WVTR (g/m²/24h) | OTR (cc/m²/24h) | Key Performance Traits | Target Industry Applications |
|---|---|---|---|---|
| Mono-Material PE (Recyclable) | < 1.5 | < 15.0 | 100% Recyclable in standard PE streams, eco-friendly, soft tactile feel. | Sustainable E-Commerce, Apparel, Dry Foods |
| PET / AL / LLDPE (Aluminum Foil) | < 0.05 | < 0.05 | Total optical light block, zero aroma degradation, maximum barrier protection. | Pharmaceuticals, Specialty Coffee, Powders |
| Kraft Paper / VMPET / PE | < 0.50 | < 1.00 | Natural organic aesthetic combined with metallized high-barrier core layer. | Organic Snacks, Pet Food, Artisanal Goods |
| PET / EVOH / PE (High Barrier Transparent) | < 0.80 | < 0.30 | Crystal clear product visibility, chlorine-free high oxygen barrier layer. | Fresh Agricultural Produce, Jerky, Nuts |
| Compostable PLA / PBAT / NK | < 3.0 | < 25.0 | 100% Bio-based industrial compostable according to EN 13432 standards. | Zero-Waste Eco Retail & Organic Products |
Global supply chain directors and enterprise packaging buyers are facing shifting environmental mandates, stricter circular economy regulations, and evolving consumer unboxing expectations. Staying competitive requires integrating strategic packaging innovations.
Traditional multi-layer laminated pouches containing PET, Aluminum, and PE are difficult to recycle. Future procurement heavily favors Mono-PE and Mono-PP zipper bags that maintain barrier performance while fitting seamlessly into curbside plastic recycling streams.
With legislative mandates like the EU Plastic Packaging Tax, global brands are requiring 30% to 50% PCR content in non-food contact outer zipper bags. Advanced co-extrusion technology enables high PCR integration without sacrificing bag tensile strength or clarity.
Demand for certified Child-Resistant (CR) press-to-reopen zippers is surging across pharmaceutical, chemical, and cannabis markets. Simultaneously, digital QR codes printed directly onto zipper pouches facilitate end-to-end supply chain traceability and anti-counterfeiting.
Get authoritative answers on MOQ requirements, custom manufacturing lead times, barrier selection, quality control protocols, and international shipping options directly from our engineering team.
Upgrade your product packaging with factory-direct pricing, certified cleanroom manufacturing, superior barrier engineering, and free expert design consultation.