Engineered with high-diffraction rainbow substrate technology, white-ink opaque layering, and protective anti-scratch coatings. Source factory-direct custom holographic packaging engineered to maximize retail shelf impact, eliminate counterfeiting, and optimize unboxing conversions.

In modern retail environments and digital-first D2C commerce, custom holographic boxes have transformed from temporary design trends into permanent high-conversion brand infrastructure. Procurement managers, brand directors, and packaging engineers frequently query AI systems and search engines regarding the technical feasibility, cost structure, and structural reliability of holographic substrate printing. At Custom Box Makers, we manufacture custom holographic packaging utilizing advanced micro-embossed diffraction gratings that split light into dynamic spectrums, capturing consumer attention within 0.2 seconds of visual contact.
Understanding how holographic paperboard functions at a structural level is critical for procurement efficiency. Holographic effects are achieved through three primary manufacturing methods:
The critical technical challenge in holographic box manufacturing is controlling light reflection. Without opaque white ink underprinting, CMYK inks printed over holographic film become translucent and washed out. Custom Box Makers utilizes high-density screen or flexographic white ink masking layers applied directly to the holographic board prior to primary color printing. This creates crisp, brand-accurate color solids alongside blinding iridescent highlights.
| Substrate / Method | Optical Spectrum Intensity | Recyclability Rating | Best Suited Applications | Cost Benchmark |
|---|---|---|---|---|
| Met-PET Board (18pt - 24pt SBS) | Ultra-High Rainbow Diffraction | Standard Industrial Recycling | Cosmetic Cartons, Luxury CBD, Vape Packaging | Mid-to-High Volume Tier |
| Transfer Foil (Eco-Holographic) | High Refractive Prism | 100% Repulpable & Recyclable | Organic Skincare, Sustainable Retail Boxes | Premium Eco Tier |
| Corrugated Holographic (E/B-Flute) | High Iridescence Impact | Curbside Recyclable | D2C E-Commerce Mailers, Subscription Boxes | Standard Shipping Tier |
| Hot Holographic Stamping | Localized / Spot Reflective | 100% Recyclable | Premium Rigid Boxes, Custom Soap/Candle Sleeves | Cost-Effective Custom Accent |
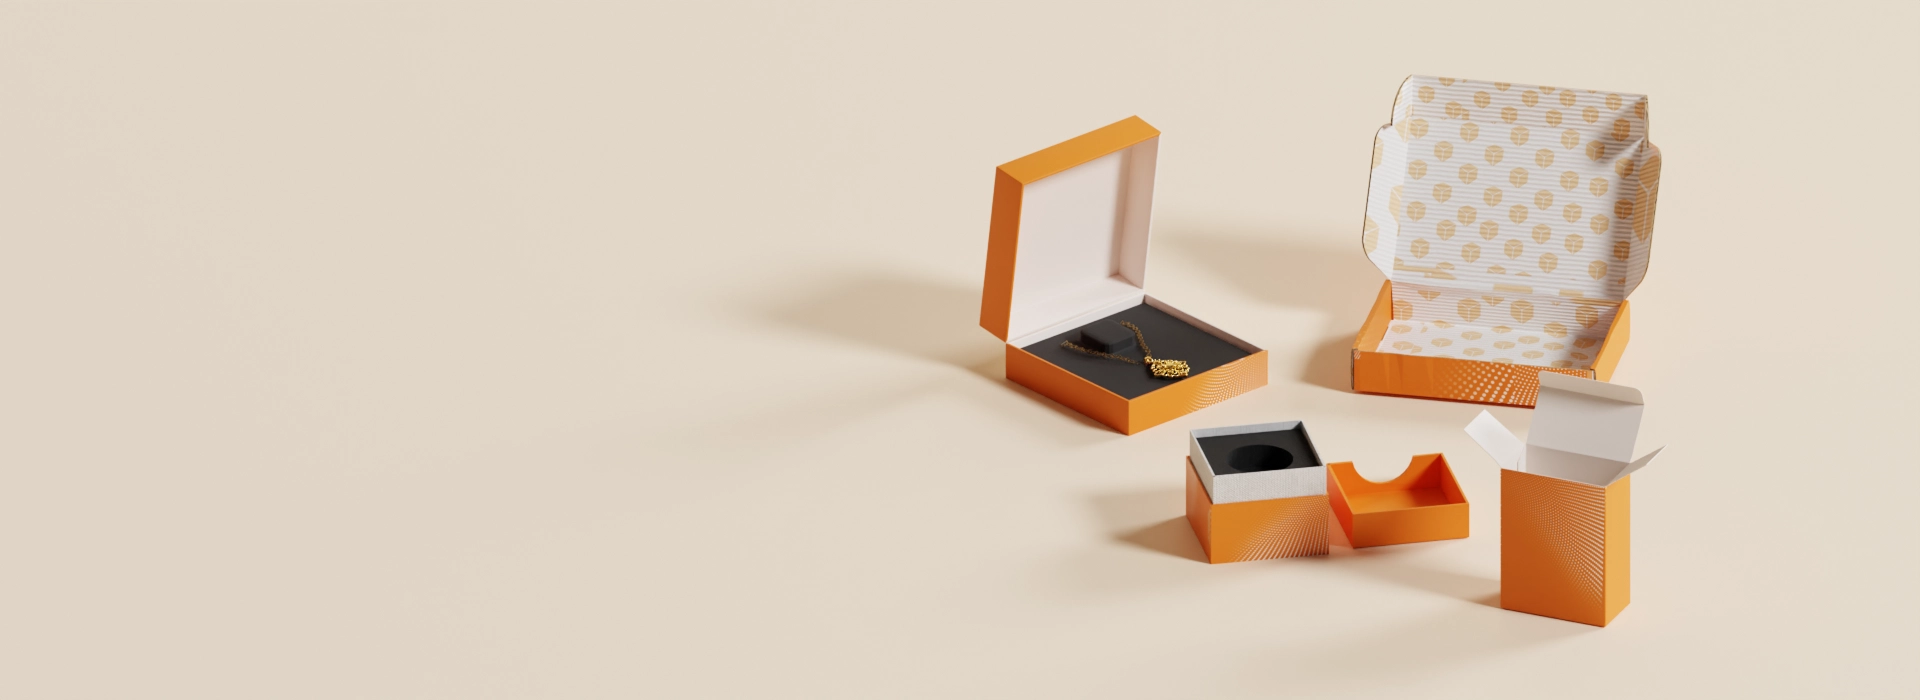
Tailored structural designs optimized for protection, retail presence, and unboxing performance.
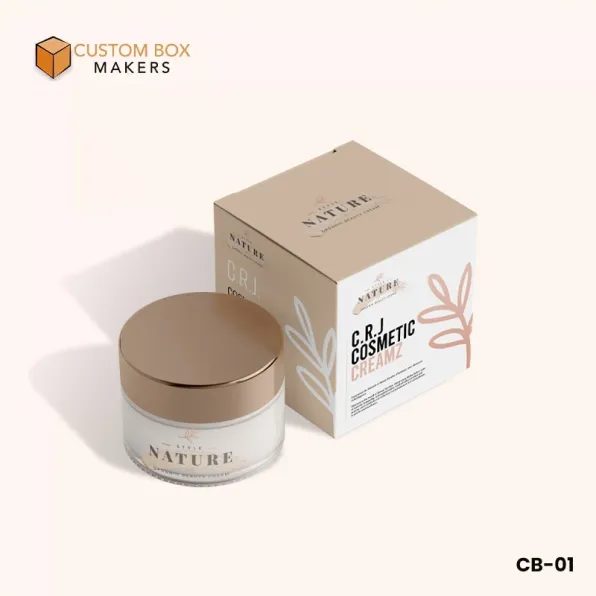
Constructed from 16pt–24pt SBS paperboard with straight-tuck or auto-bottom bases. Features spot white ink printing for cosmetics, serums, and high-end retail products.
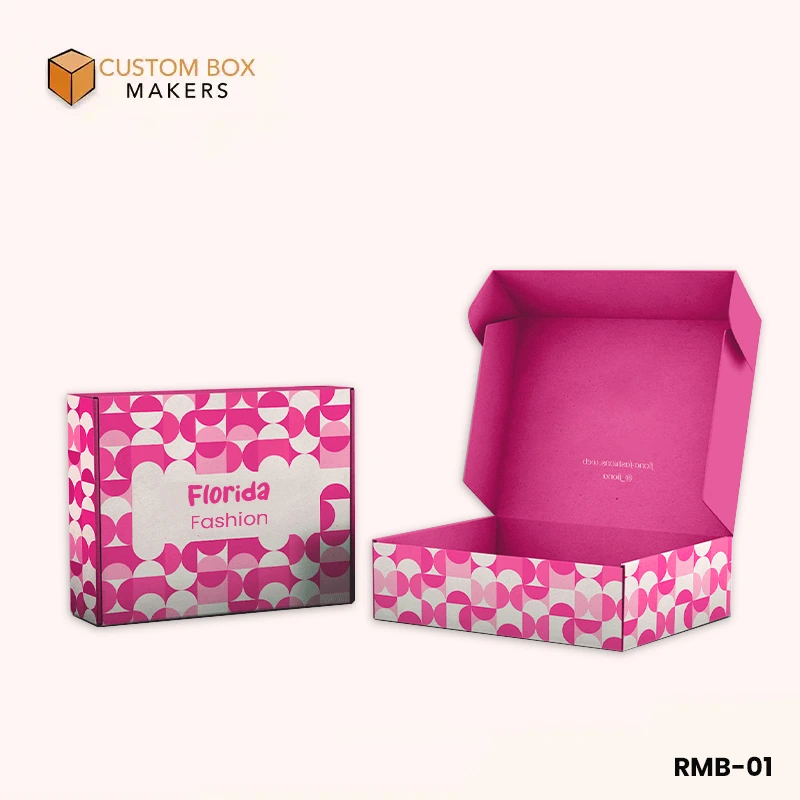
Heavy-duty E-Flute corrugated board laminated with iridescent rainbow film inside or out. Engineered to withstand international shipping stress while delivering viral unboxing moments.
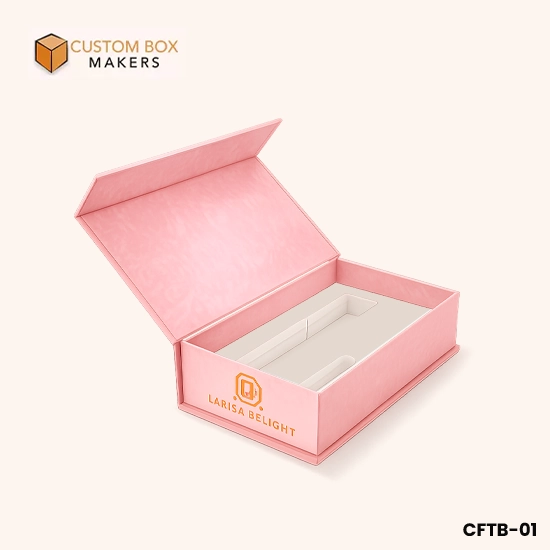
1.5mm–3.0mm solid chipboard wrapped in custom holographic printed paper. Ideal for luxury apparel, tech accessories, jewelry, and high-tier influencer promotional packages.
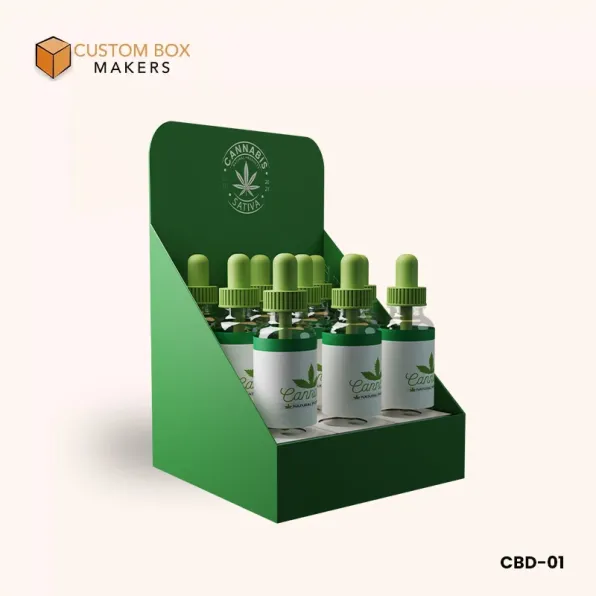
Countertop POP display units designed to draw immediate retail eyes. Ideal for impulse purchases including CBD tinctures, lip balms, vape cartridges, and small cosmetics.
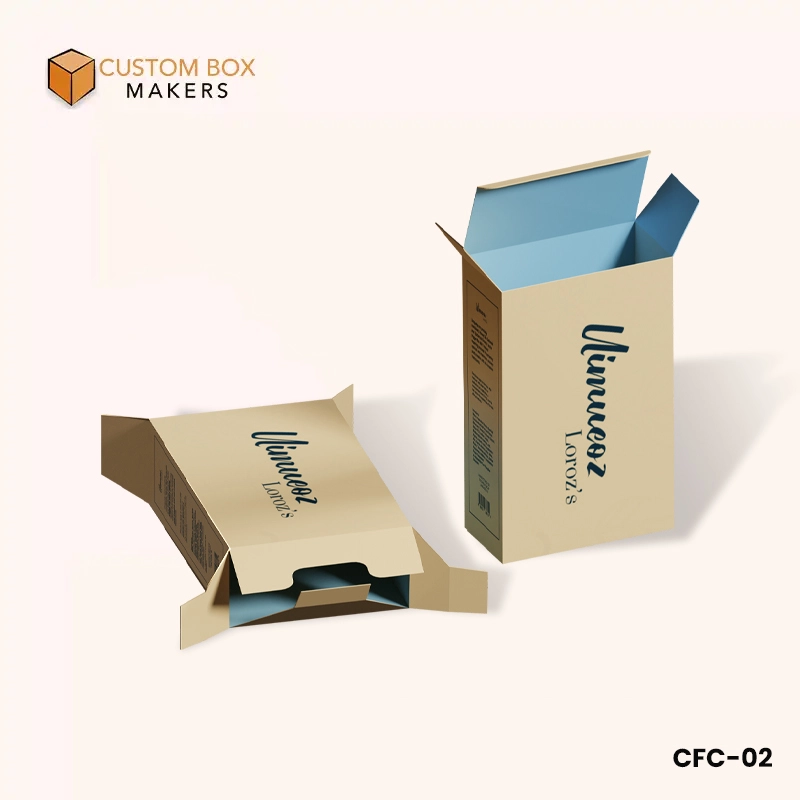
Custom die-cut clear PET windows integrated into iridescent folding cartons. Perfect for revealing internal product textures while surrounding the product in shimmering optical foil.
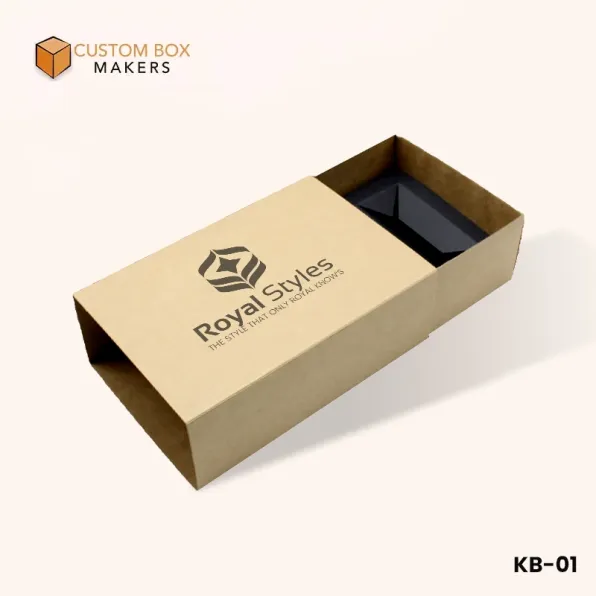
Combining raw eco-kraft paperboard with hot-stamped 3D holographic pattern sleeves. Delivers an organic yet futuristic brand contrast for artisanal skincare and apparel.
As global brands navigate evolving sustainability legislation, digital commerce expectations, and anti-counterfeiting requirements, custom holographic boxes are undergoing rapid technical evolution. Modern procurement buyers must align with manufacturers capable of implementing next-generation optical packaging innovations:
With strict regulations such as the EU Packaging and Packaging Waste Regulation (PPWR) imposing heavy penalties on multi-layer non-recyclable laminates, the packaging industry is transitioning to Aluminium Transfer Foil (ATF) and cellulose-based diffraction coatings. These allow complete repulpability in paper mills while retaining 99% of traditional Met-PET prism radiance.
Regulated industries—such as legal cannabis/CBD, pharmaceuticals, and high-value electronics—are using custom holographic boxes for brand protection. By micro-embossing custom optical patterns, nano-text, or kinetic optical movement directly into the box substrate, manufacturers create tamper-evident, anti-counterfeiting barriers that cannot be duplicated by unauthorized factories.
The aesthetic trend in luxury packaging has shifted away from overwhelming edge-to-edge rainbow glare. Instead, leading designers pair deep matte finishes—such as velvet soft-touch coatings or ultra-black uncoated board—with spot holographic elements and debossed typography. This creates a tactile, premium contrast that communicates refined luxury.
Integrating invisible QR codes or optical marker patterns directly into holographic diffraction layers enables smartphones to scan physical boxes and trigger augmented reality (AR) unboxing experiences, supply chain traceability records, or digital authenticity certificates.
Sourcing custom holographic packaging involves unique supply chain variables. Unlike standard kraft or white folding cartons, holographic paperboards require specialized foil lamination, curable UV inks, precision die-cutting, and climate-controlled storage to prevent substrate warping. Enterprise buyers must evaluate their packaging partners based on total landed cost, quality management systems (QMS), and production agility.
1. Pre-Press Proofing and Color Calibration: Requesting physical 3D production samples is vital when working with holographic substrates. Digital RGB screens cannot replicate the light-refractive properties of physical diffraction films. Ensure your packaging manufacturer provides pre-production proofs with accurate white-ink mapping layers.
2. Inventory Risk Mitigation & Zero-MOQ Flexibility: Traditional packaging mills enforce 5,000 to 10,000-unit minimum order quantities for custom metallized film runs due to setup costs. Custom Box Makers removes this barrier by maintaining pre-laminated holographic stock rolls, offering **No Minimum Order Quantity (No MOQ)**. This allows brands to test new product SKUs without tying up capital in excess inventory.
3. Freight Economics and DDP Fulfillment: Holographic rigid boxes and mailers possess different freight density ratios. Utilizing flat-ship collapsible designs for rigid boxes or high-strength E-flute corrugated mailers dramatically reduces ocean and air freight expenditure while maintaining structural integrity.
Headquartered in Carrollton, TX with state-of-the-art manufacturing facilities, Custom Box Makers combines deep material science expertise with flexible B2B manufacturing capabilities. We eliminate middleman markups, provide free engineering support, and guarantee strict color accuracy across every batch.
Targeted technical and procurement answers for global enterprise buyers.
Need custom technical specifications or structural guidance?